GFRPINDIA
The machines

Five lines. One of them is probably yours.

Physical specification and what sits inside each line. Output figures and prices come with a conversation, not from a web page.
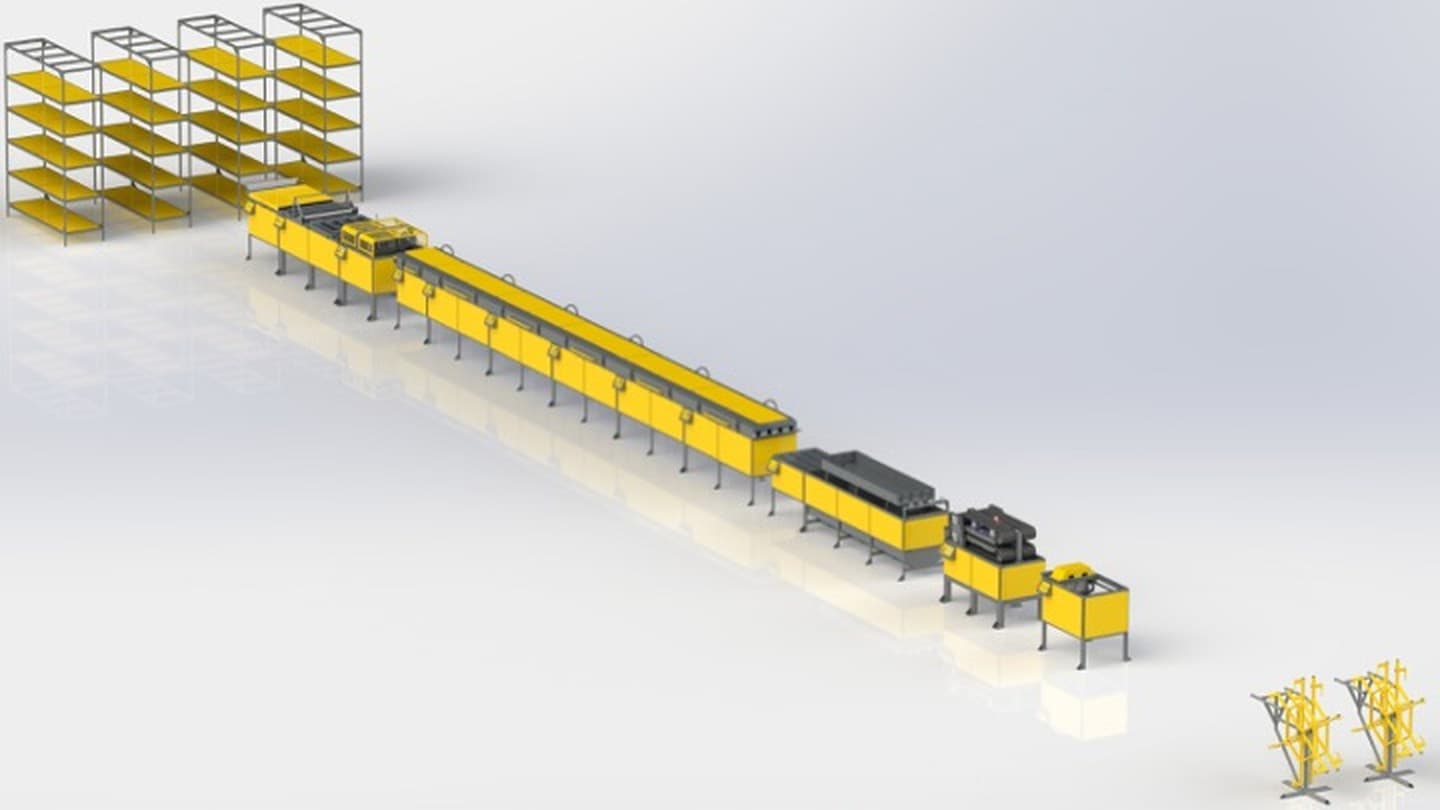
Composite Tech GFRP rebar production line, full layout from rack to outputFull line layout · rack to finished bar

CT2

Straight rebar · two bars

The entry line. Smallest footprint of the three and the usual starting point for a plant running one or two diameters.

2Bars at once
3–20 mmDiameter range
3-phaseSupply
CaterpillarPuller type

CT4

Straight rebar · four bars

The common choice. Enough line for a plant selling into private work with room to take a bigger order.

4Bars at once
3–20 mmDiameter range
31.5 × 5.2 × 2.5 mFootprint L×W×H
CaterpillarPuller type

CT6

Straight rebar · six bars

What we run at Pithampur. Same footprint as the CT4, more bars through it.

6Bars at once
3–20 mmDiameter range
35 kWConnected power
380 V3-phase supply

CNC bent

Bent elements

Stirrups and shaped elements, cut and bent to drawing. Different economics from straight bar, usually better.

6–16 mmDiameter range
CNCBending control
ProgrammableShape memory
Separate lineNot an attachment

CT1M / CT2M

Mesh

Welded GFRP mesh for slabs and surface beds.

1 or 2Mesh widths
ProgrammableGrid spacing
Roll or sheetOutput form
Separate lineNot an attachment

Inside the line

Eight stations in a row. Each one can spoil what the one before it did, which is why a four-hour run tells you more than a specification sheet.

01CreelRoving feeds from racks at the back of the line. How evenly it feeds decides whether the bar holds a consistent section.
02Roving dryerDrives moisture out before the fibre meets resin. Moisture at this point is a defect you cannot see until the bar is tested.
03Impregnation moduleResin introduced in stages rather than one bath. Dry fibre left inside a bar is a void, and voids are where alkali attack starts.
04Twisting and ribbingHelical wrap and surface applied before cure. Whether rib distance can be changed, and stays synced to pulling speed, decides how much of your day goes on resetting the line.
05Curing · infrared boosterShort-wave infrared passes through the glass and is absorbed by the resin, so the bar begins curing from the inside out.
06Curing · tunnel kilnConventional curing follows the booster. The two together are the curing section, and the kiln is where heaters either hold 250 °C or fade.
07Cooling moduleControlled cooling. Too fast and you lock stress into the bar.
08Pulling deviceGrips along a length rather than at points. This is what holds tolerance, and where you watch for slippage on a multi-bar run.
09Cutting deviceTo length, automatically. Manual measure means a man, a tape, and a variance you will argue about with customers.
10WinderCoiled for despatch. Compact coils or large ones — large coils cost you more to ship, to every customer, for the life of the plant.

The lines also run basalt and carbon fibre, and epoxy, vinyl ester or polyester resin systems.